Blog

2026 Best Harness Wire Types for Global Buyers?

Choosing the right harness wire is a practical decision, not a simple product comparison. Global buyers must evaluate conductor material, insulation, temperature rating, flexibility, voltage, and installation conditions. A wire designed for a dry passenger cabin may fail quickly inside an engine compartment. Heat, vibration, oil, moisture, bending, and repeated movement all change performance.

Markus Schmid, a veteran wiring-harness engineer, puts the decision plainly: “The best harness wire is the one that survives its actual environment.” That principle sounds obvious. It is often ignored. Buyers may focus on price, color, or delivery speed while overlooking insulation aging and terminal compatibility. Copper remains widely selected for its conductivity and reliable crimping behavior. Aluminum can reduce weight, but it demands careful joint design and corrosion control. Tinned copper may offer stronger resistance in humid or marine environments.

This guide examines the best harness wire types for global buyers in 2026. It considers automotive, industrial, renewable-energy, robotics, and heavy-equipment applications. Each section connects wire construction with real installation risks. We will compare PVC, XLPE, cross-linked insulation, shielded designs, and high-flex options. The analysis also addresses documentation, traceability, testing, and supplier consistency across regions.

There is no universal winner. Even experienced engineers can choose poorly when field conditions are incomplete. A flexible silicone wire may perform well near moving parts, yet become unnecessary for a fixed indoor assembly. Buyers should question every recommendation, verify specifications, and request samples before large orders. Cost still matters. Reliability matters more.
2026 Best Harness Wire Types for Global Buyers?

Harness Wire Types: Definition, Structure, and Core Functions

2026 Best Harness Wire Types for Global Buyers?

Harness Wire Types: Definition, Structure, and Core Functions

A wiring harness is an engineered group of wires that carries power and data between components. It combines conductors, insulation, terminals, seals, clips, and protective sleeves. Its structure guides current through a controlled route. Stranded copper wire handles vibration well and remains easy to crimp. Aluminum wire lowers weight but requires careful joint design and corrosion control. Shielded twisted-pair wire limits electromagnetic noise around communication circuits. Coaxial cable suits high-frequency signals, while high-voltage cable needs thick insulation and clear identification. Short runs differ.

Core functions include power delivery, signal transmission, grounding, protection, and service organization. In vehicles, insulation must resist heat, oil, moisture, and repeated movement. In factory equipment, fine-strand wire often tolerates robotic motion better.

The International Energy Agency reported nearly 14 million electric car sales in 2023, representing about 18% of global car sales. This shift increases demand for high-voltage conductors, shielding, and reliable temperature ratings. The OICA 2023 production report recorded more than 93.5 million motor vehicles worldwide.

For global buyers, that scale makes standardization important. Regional voltage rules, testing methods, and terminal geometries still vary. A practical specification should name conductor material, cross-sectional area, insulation rating, bend radius, shielding, and test standard. Do not choose by color alone. A neat classification helps, but it is not perfect. Actual routing, load peaks, installation skill, and repair access can change the best choice.

Main Materials Used in Harness Wire Manufacturing

2026 Best Harness Wire Types for Global Buyers?

Main Materials Used in Harness Wire Manufacturing

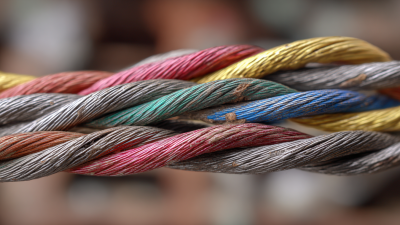
Copper remains the practical choice for most harness wires. It carries current efficiently and bends without cracking during assembly. Bare copper works well in controlled environments. Tinned copper adds a protective layer against moisture and oxidation. This matters in engine compartments, outdoor equipment, and humid factories. However, tin plating adds cost and can affect crimping behavior.

Aluminum offers lower weight and material cost. Its larger conductor size can offset some space savings. Copper-clad aluminum reduces weight further, but buyers should examine conductivity, flexibility, and terminal compatibility carefully. A cheaper conductor may create higher resistance and installation problems. That trade-off is easy to underestimate.

Insulation materials shape daily performance. PVC is economical and suitable for many indoor harnesses. Cross-linked polyethylene tolerates greater heat and abrasion. Silicone stays flexible in cold conditions, although it can tear more easily. Thermoplastic polyurethane resists oil and repeated movement. I have found that material selection often fails when buyers compare only voltage ratings. Temperature cycling, bend radius, wall thickness, and crimp quality deserve equal attention. No material wins every application. A small sample test can reveal issues that a datasheet misses.cuntegn

Key Harness Wire Types for Different Global Applications

2026 Best Harness Wire Types for Global Buyers?

Key Harness Wire Types for Different Global Applications

Harness wire selection depends on temperature, movement, chemicals, voltage, and installation space. A low-cost choice can fail quickly in a hot engine compartment. PVC-insulated wire suits many indoor controls and general equipment. It offers flexibility, clear color coding, and practical cost control. However, PVC may soften near persistent heat or oil exposure.

XLPE wire performs better in high-temperature automotive and industrial harnesses. Its insulation resists heat, abrasion, and several common fluids. ETFE wire supports compact aerospace, medical, and instrumentation assemblies. Its thin insulation saves space without sacrificing strong dielectric performance. Silicone wire remains useful where repeated bending occurs, such as robotic arms and movable panels. It feels soft. That helps.

Signal-heavy applications often need shielded twisted-pair wire. The twisted conductors reduce electromagnetic interference between sensors and control units. Coaxial harness wire may suit cameras, antennas, and high-frequency measurement systems. Thermocouple wire requires matching conductor materials and correct polarity. A small mistake can distort temperature readings.

During sourcing, I check conductor strand count, insulation diameter, bend radius, and terminal compatibility. I also request crimp pull-test data and sample assemblies. A datasheet alone is not enough. Field conditions often differ from laboratory assumptions. I once reviewed a harness that passed electrical testing but failed after repeated bending. The design ignored routing stress. Buyers should verify regional markings, environmental ratings, and production consistency before approving a global supplier. Some projects still need revision after the first sample.

2026 Best Harness Wire Types for Global Buyers?

Key harness wire types for different global applications, compared by representative maximum continuous conductor-temperature class.

FLRY-B is widely used for compact low-voltage automotive harnesses. TXL and GXL are suitable for engine-compartment and general vehicle wiring, while SXL is selected where thicker insulation and higher mechanical durability are required. ISO 19642 Class D high-voltage cable is designed for demanding electric-vehicle power systems. Final selection should also verify voltage, current capacity, conductor cross-section, flexibility, shielding, chemical resistance, and the destination-market standard.

International Standards, Safety Ratings, and Quality Requirements

Global buyers should select harness wire by application, not catalog appearance. In automotive systems, thin-wall PVC often suits moderate heat and controlled interiors. XLPE handles higher temperatures and tighter routing with better insulation stability. Silicone remains flexible in cold conditions, but its abrasion resistance may need verification. For severe heat or chemicals, fluoropolymer insulation can be appropriate, although cost and processing demands increase. Temperature matters.

International standards create a common testing language, but they do not remove purchasing risk. Check conductor construction against IEC 60228 where applicable, and confirm performance under the target market’s requirements. Automotive projects may reference ISO 6722 for dimensions, temperature classes, and electrical performance. Safety reviews should cover voltage rating, flame behavior, dielectric strength, insulation resistance, oil exposure, vibration, and abrasion. IP protection belongs to the connector and enclosure system, not the wire alone. That detail is often missed. Require RoHS and REACH declarations when relevant, with controlled material records.

Reliable suppliers provide drawings, batch numbers, test reports, and samples from regular production. Inspect crimp pull force, terminal retention, conductor stranding, insulation thickness, and color consistency. A clean sample can hide unstable production. Incoming checks should include cross-sections and resistance testing for critical circuits. Do not accept “equivalent” material without comparing temperature, wall thickness, flexibility, and chemical data. Requirements can conflict. A softer jacket may improve routing but reduce cut resistance. Specifications also deserve annual review because field temperatures, assembly tools, and certification expectations can change. Small gaps become expensive failures.

2026 Best Harness Wire Types for Global Buyers? — International Standards, Safety Ratings, and Quality Requirements
Wire Type / Insulation Typical Temperature Capability Typical Voltage Range Key Performance Advantages Common Harness Applications Relevant International Standards Safety and Quality Requirements for Buyers
PVC-Insulated Hook-Up or Automotive Wire Commonly 80°C to 105°C; higher-temperature grades are available. Commonly 60 V, 300 V, or 600 V, depending on construction and certification. Cost-effective, flexible, widely available, and easy to process. Provides good abrasion and chemical resistance for general-purpose harnesses. Appliances, control panels, low-voltage vehicle circuits, industrial equipment, and general internal wiring. IEC 60227 for certain PVC-insulated cables; ISO 6722 for many road-vehicle cables; UL 758 for recognized appliance wiring constructions; IEC 60332-1-2 for applicable vertical flame testing. Confirm conductor class, insulation thickness, temperature rating, voltage rating, flame performance, RoHS/REACH status, and lot traceability. PVC is not suitable for every high-temperature or high-voltage environment.
XLPE-Insulated Automotive Wire Typically 125°C to 150°C for automotive constructions; the exact rating must be verified on the cable specification. Commonly 60 V or 600 V in road-vehicle cable families, depending on the applicable design. Higher thermal capability than standard PVC, good resistance to automotive fluids, strong abrasion resistance, and relatively thin insulation for weight and space savings. Engine compartments, battery circuits, chassis harnesses, electric vehicles, and high-temperature industrial equipment. ISO 6722 and ISO 19642 for road-vehicle cable requirements; SAE J1128 for applicable automotive wire constructions; IEC 60332-1-2 where flame testing is specified. Check long-term temperature index, conductor flexibility, insulation stripping performance, oil and fuel resistance, bend radius, voltage class, and compatibility with crimp terminals.
ETFE-Insulated Wire Often rated approximately −65°C to +150°C or higher, depending on the construction and qualification. Commonly 300 V or 600 V; aerospace and specialized constructions may use different ratings. Very thin, lightweight, highly abrasion-resistant, and resistant to many chemicals, fuels, and solvents. Supports compact harness designs. Aerospace equipment, defense electronics, high-density instrumentation, robotics, and demanding industrial harnesses. AS22759 for many aerospace wire constructions; applicable ASTM, EN, or customer-specific aerospace specifications; UL 758 for applicable appliance wiring constructions. Require documented conductor plating, insulation identification, dimensional control, dielectric withstand results, abrasion testing, and batch-level certificates. Verify whether the application permits ETFE processing and termination methods.
FEP-Insulated Wire Often approximately −65°C to +200°C, depending on the product design. Commonly 300 V or 600 V for commercial constructions. Excellent chemical resistance, low friction, low moisture absorption, and reliable performance at elevated temperatures. Laboratory instruments, chemical-processing equipment, aircraft systems, heaters, and high-temperature control harnesses. UL 758 for applicable appliance wiring; ASTM and aerospace specifications for specialized constructions; IEC or EN requirements may apply to the completed cable or equipment. Confirm insulation wall thickness, cold-bend performance, dielectric strength, smoke or flame requirements, conductor plating, and compatibility with soldering or crimping processes.
Silicone-Insulated Wire Commonly approximately −60°C to +180°C; some constructions are rated higher or lower. Commonly 300 V or 600 V, subject to the product certification. Excellent flexibility over a wide temperature range, good resistance to heat and cold, and good vibration tolerance. Medical devices, lighting, heaters, battery packs, laboratory equipment, robotics, and flexible moving harnesses. UL 758 for applicable appliance wiring constructions; IEC 60245 for certain rubber-insulated cable categories; IEC 60332 or equivalent flame tests where required. Evaluate tear and abrasion resistance, oil compatibility, termination pull force, insulation compression, flame rating, particle contamination, and whether silicone residue could affect connectors or sensors.
Cross-Linked Polyolefin Wire Commonly 105°C to 125°C; specialized versions may provide higher ratings. Often 60 V or 600 V in automotive and equipment wiring designs. Good balance of flexibility, abrasion resistance, chemical resistance, reduced wall thickness, and low smoke compared with some conventional materials. Automotive harnesses, battery systems, industrial controls, appliances, and compact equipment assemblies. ISO 6722 or ISO 19642 for applicable road-vehicle cables; SAE J1128 for relevant automotive constructions; IEC 60332-1-2 where applicable. Verify material formulation, thermal aging, fluid resistance, conductor stranding, insulation recovery after stripping, flame behavior, and compatibility with automated cut-and-strip equipment.
PUR-Insulated Cable Typically approximately −40°C to +80°C or +90°C; high-temperature grades vary by formulation. Commonly 300 V or 600 V for industrial cable constructions. Excellent abrasion, flexing, oil, and mechanical resistance. Suitable for repeated movement and harsh industrial environments. Robotics, drag chains, machine tools, automated production lines, and mobile industrial equipment. EN 50525 and applicable European cable requirements; UL 758 or UL industrial cable requirements where certified; IEC 60332 where flame performance is specified. Check bending-cycle rating, minimum dynamic bend radius, torsion performance, oil resistance, shielding effectiveness, conductor fatigue life, and connector overmolding compatibility.
Shielded Twisted-Pair Harness Cable Determined by the conductor insulation and jacket system; common industrial ratings are 80°C to 105°C. Often 30 V to 300 V for signal and communication circuits; power versions may be rated differently. Twisting controls electromagnetic interference, while shielding improves noise immunity and signal integrity. CAN, Ethernet, sensors, industrial automation, medical equipment, instrumentation, and data communication harnesses. ISO 11898 for CAN physical-layer applications; IEC 61156 for applicable balanced communication cables; ISO/IEC 11801 for relevant structured cabling performance. Specify impedance, pair lay length, capacitance, attenuation, shield coverage, drain-wire design, pair-to-pair crosstalk, termination method, and EMC test conditions.
High-Voltage EV Cable Commonly 125°C to 150°C, with higher-rated constructions available for specific zones. Commonly 600 V DC or 1,000 V DC class in electric and hybrid vehicle systems; the exact rating depends on the cable and vehicle architecture. Designed for high-voltage battery, inverter, motor, and charging circuits, often with enhanced insulation, shielding, and orange identification. Electric vehicles, hybrid vehicles, charging systems, battery storage, and high-voltage power electronics. ISO 19642 for road-vehicle cables; ISO 6469 for relevant electric road-vehicle safety requirements; LV 216 for applicable automotive high-voltage cable specifications; IEC 60664 principles may support insulation coordination. Require touch-safe design, insulation resistance, dielectric withstand, partial-discharge or high-voltage testing where specified, shield continuity, orange identification, HVIL compatibility, thermal aging, and traceable crimp validation.
Halogen-Free Low-Smoke Wire Often 70°C to 125°C, depending on the insulation and cable category. Commonly 300 V, 450/750 V, or 600 V depending on the applicable standard. Reduced corrosive halogen emissions and lower smoke generation during fire compared with many PVC-based constructions. Public transportation, buildings, control cabinets, data facilities, tunnels, and safety-critical indoor installations. IEC 60754 for halogen-acid gas assessment; IEC 61034 for smoke density; IEC 60332 series for flame propagation; EN 50575 for construction-product fire performance where applicable. Do not treat “halogen-free” as a complete fire rating. Verify smoke, flame spread, heat release, toxicity requirements, voltage rating, bending behavior, and local installation regulations.
Buyer verification note: Ratings shown are typical ranges, not universal guarantees. The final selection should be based on the exact cable construction, conductor size, installation environment, applicable country regulations, certification scope, terminal system, and completed-harness validation results.

How Global Buyers Compare and Select Harness Wire Types

Global buyers compare harness wire types by matching the insulation to the working environment, not by choosing the lowest price. Start with the environment. A PVC-insulated wire may suit indoor equipment and moderate temperatures. XLPE supports higher heat and better chemical resistance. PTFE and ETFE perform well in compact assemblies exposed to heat, oils, or aggressive fluids. They usually cost more and may require different processing tools.

Engineers should check conductor size, strand flexibility, voltage rating, temperature range, bend radius, flame behavior, and abrasion resistance. A thick jacket can feel safer, but it may make routing difficult inside a crowded control cabinet. Fine-stranded copper improves flexibility, while larger conductors reduce voltage drop over long harnesses. Material choice affects weight, too. That matters in vehicles, robotics, and aircraft systems.

Reliable buyers compare complete datasheets, inspection reports, batch traceability, and relevant international test evidence. They also request samples before approving volume production. Pull tests, insulation checks, bending cycles, and heat-aging tests can reveal weaknesses hidden by attractive specifications. Supplier audits add useful evidence, especially when production crosses borders. One practical issue is often underestimated: the same wire may behave differently after crimping, bundling, and repeated movement. Selection is not perfect on paper. A short pilot build can expose that mistake early.

Go to Top